2026 Top ASME Reactor Manufacturers for Global Buyers?
Choosing the right reactor manufacturer in 2026 requires more than comparing prices or browsing polished websites. Global buyers need verified engineering capability, documented quality systems, and dependable project communication. This guide examines leading Asme Reactor manufacturers through practical purchasing criteria. These include design experience, pressure-vessel expertise, material traceability, welding control, inspection access, and after-sales support.
A capable manufacturer should understand the reactor’s actual working conditions. Temperature, pressure, corrosive media, agitation speed, and cleaning procedures all influence the final design. Buyers should review ASME certification scope, applicable BPVC requirements, inspection records, and fabrication examples. A stainless steel reactor may look excellent in a factory photograph. Its weld map and surface finish matter more. So does the supplier’s response when specifications change.
Details reveal competence.
This overview is not a permanent ranking. Market performance, certifications, production capacity, and delivery reliability can change during 2026. Some suppliers communicate impressively but provide limited technical evidence. Others have strong workshops yet weak export coordination. That difference deserves closer attention. We will consider manufacturers with relevant experience, transparent documentation, and realistic delivery commitments. Independent verification remains essential before signing any contract. Buyers should confirm certificates directly, clarify testing responsibilities, and compare warranty terms carefully. No single manufacturer fits every application, especially when pharmaceutical, chemical, food, or research requirements differ. The strongest choice balances compliance, engineering judgment, lifecycle cost, and responsive human support. Mistakes still happen, even among experienced suppliers. A careful process reduces their impact.
2026 ASME Reactor Market: Capacity, CAGR, and Global Buyer Demand Data
2026 Top ASME Reactor Manufacturers for Global Buyers?
The 2026 ASME reactor market is expanding with global demand from pharmaceuticals, specialty chemicals, food processing, and battery materials. Industry estimates place annual market growth near 6% to 8%, although regional reporting methods differ. Numbers vary.
Fabrication capacity remains concentrated among qualified pressure-vessel producers. Indicative global capacity may reach 1.8 to 2.3 million vessel-equivalent units by 2026. Many established workshops report booking levels between 65% and 80%.
Standard reactors may require eight to fourteen months, while jacketed or high-alloy designs often need longer schedules.
Buyers should verify capacity through production plans, not brochures.
Practical procurement reviews focus on ASME certification scope, material traceability, weld procedures, inspection records, and pressure-test documentation.
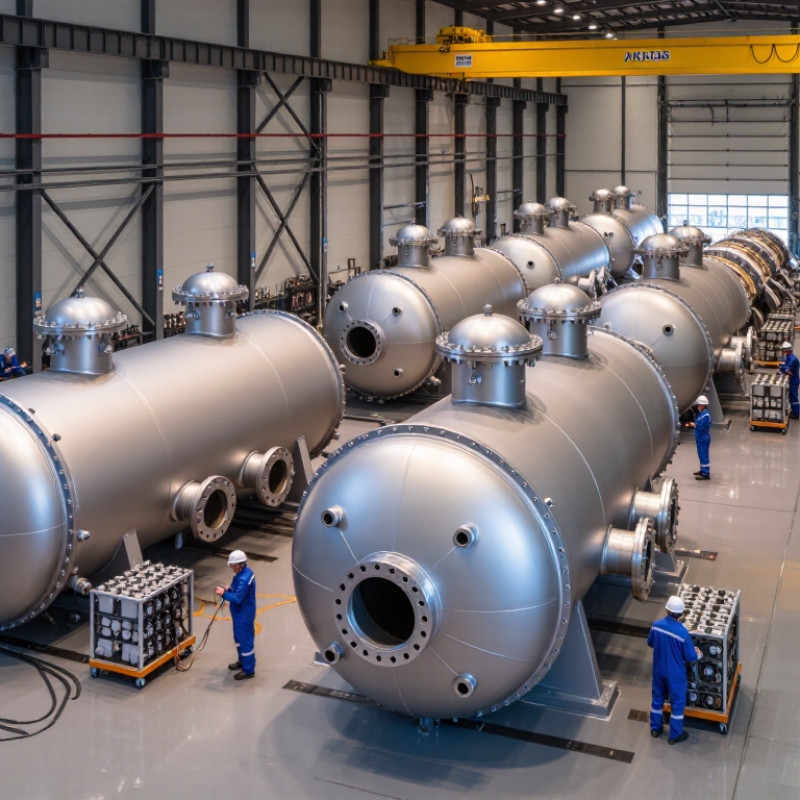
A reliable supplier should provide drawings showing shell thickness, nozzle orientation, agitator clearance, and heating-zone coverage. These details affect installation costs and operating stability.
Demand is strongest for stainless steel and corrosion-resistant reactors, especially in Asia, North America, and the Middle East.
Yet CAGR figures can mislead when they combine small pilot units with large industrial vessels.
I have seen projects delayed because market reports ignored local inspection rules, port limits, or spare-part access.
Buyer forecasts should therefore separate capacity, order value, vessel size, and actual delivery performance.
Top Manufacturers Ranked by 5 Metrics: Quality, Capacity, Lead Time, Cost, Exports
2026 Top ASME Reactor Manufacturers for Global Buyers
For global buyers, an ASME reactor ranking should measure more than certificate ownership. Quality begins with documented welding procedures, qualified inspectors, material traceability, and complete non-destructive examination records. Shop-floor discipline matters too. A clean fabrication bay often reveals more than polished sales language.
Capacity
Capacity is measured through active projects, vessel size, alloy handling, and production scheduling. Lead time should include design review, procurement, fabrication, inspection, and export packing. A quoted delivery date means little without milestone evidence. Request a production schedule with inspection hold points. Delays often start with late drawings or unavailable specialty materials.
Cost
Cost requires a wider lens. Compare fabrication price, testing, transport, installation support, spare parts, and future maintenance. The lowest offer may carry expensive uncertainty.
Export performance
Export performance adds another useful metric: completed international shipments, packing quality, customs documentation, and experience with destination requirements. Ask for anonymized project records and recent inspection reports. That is practical evidence.
No ranking is perfect. Capacity can change quickly. A strong factory may still miss a delivery window during a material shortage. Buyers should score each manufacturer against the same five metrics, then verify claims through audits, reference checks, and technical meetings. Independent review remains valuable, especially when commercial pressure affects judgment.
Reactor Material Benchmarks: 316L, Hastelloy, Titanium, and Glass-Lined Steel
For global buyers comparing ASME reactor manufacturers in 2026, material selection deserves more attention than catalog capacity. The vessel must match chemistry, temperature, pressure, cleaning methods, and maintenance access. An ASME stamp confirms code construction, not universal corrosion resistance.
316L stainless steel remains practical for many aqueous processes. Its smooth surface supports hygienic cleaning, while its cost is often manageable. However, chlorides, low-pH mixtures, and stagnant zones can cause pitting. I have seen a polished vessel fail early because operators underestimated concentration changes. Small details matter.
Hastelloy offers stronger resistance in aggressive chemical service, but its purchase price and fabrication requirements are higher. Titanium performs well against many chlorides and seawater-related environments, yet hydrogen absorption, crevice conditions, and welding controls require careful review. It is not automatically the safest choice. Glass-lined steel provides excellent chemical resistance and a clean process surface, especially for batch reactions. Its glass layer can suffer from impact, thermal shock, or poor transport handling. Inspectors should check spark-test records, lining thickness, nozzle areas, and repair history.
A reliable supplier should provide material certificates, weld procedures, pressure-test documentation, and traceable inspection records. Ask how the manufacturer validates agitator seals and internal coils, not only the shell. Real operating data is more useful than broad corrosion charts. The final selection should reflect the actual process recipe, including unexpected contaminants and cleaning cycles.
2026 Material Benchmarks for ASME Reactor Buyers
Representative engineering values for common reactor construction materials. Density is shown in kg/m³, while thermal conductivity is shown in W/m·K. For glass-lined steel, density refers to the steel substrate and thermal conductivity refers to the glass corrosion barrier.
Typical reference values: 316L stainless steel, Hastelloy C-276, commercially pure Titanium Grade 2, and glass-lined carbon steel. Actual ASME vessel selection depends on pressure, temperature, chemical compatibility, lining design, fabrication quality, and project-specific code calculations.
Global Compliance Checklist: PED 2014/68/EU, ISO 9001, FAT, and Traceability
Global buyers comparing ASME reactor manufacturers in 2026 should treat compliance evidence as a purchasing filter, not a brochure claim. For equipment placed on the EU market, PED 2014/68/EU requires hazard classification, essential safety requirements, and an appropriate conformity assessment route. ASME Section VIII supports pressure-vessel design, but it does not automatically replace PED obligations. That distinction is often missed.
ISO’s 2023 Survey reported 1,265,216 ISO 9001 certificates worldwide. Certification helps, but it cannot verify every weld or material certificate. Request the current certificate scope, audit status, and corrective-action records. The manufacturer should also provide design calculations, approved drawings, weld procedures, welder qualifications, and non-destructive examination results. Check the details.
During FAT, buyers should witness hydrostatic or pneumatic testing, alarm checks, agitator rotation, instrument calibration, and document review. A practical FAT dossier includes calibrated-gauge certificates, test pressures, acceptance criteria, punch-list closure, and signed attendance records. Testing conditions should reflect the reactor’s operating envelope, not an easy demonstration setting.
Traceability must continue from raw plate to final vessel. Heat numbers should match material certificates, weld maps, and inspection reports. Digital records reduce manual errors, although poor data entry can still create false confidence. Industry quality studies repeatedly identify documentation gaps as a major source of project delay; therefore, require a searchable manufacturing record book before shipment, not after installation. Check revision control carefully.