How to Choose an Alcohol Recovery Tower for Your Plant
Choosing an Alcohol Recovery Tower is a process decision, not simply an equipment purchase. Its performance affects product quality, solvent losses, steam demand, and the stability of downstream operations. The International Energy Agency’s Energy Efficiency 2023 report puts industry’s share at roughly 37% of global final energy consumption. That figure makes energy use a practical design concern, not a detail to check after installation. Small details matter.
The U.S. Department of Energy’s Bandwidth Study on Energy Use and Potential Energy Savings Opportunities in U.S. Chemical Manufacturing identifies distillation as an important area for energy-efficiency improvements. Yet a tower that looks efficient on paper may struggle with a changing feed, variable alcohol concentration, or limited turndown. Selection should begin with measured feed composition, flow range, operating pressure, recovery target, and product specifications. Engineers should also review vapor-liquid equilibrium data, condenser and reboiler duties, corrosion risks, and available utilities. Field data wins.
A useful comparison weighs total operating cost against purchase price. Packing or trays, column diameter, insulation, controls, and maintenance access can each affect performance and uptime. No single configuration suits every plant. Pilot results and vendor guarantees deserve scrutiny, especially when feed data is incomplete. That uncertainty is worth stating plainly. The right Alcohol Recovery Tower is the one sized for real operating conditions, with assumptions documented and performance verified against plant needs.
Characterize Feed Composition, Including Water, Solids, and Trace Impurities
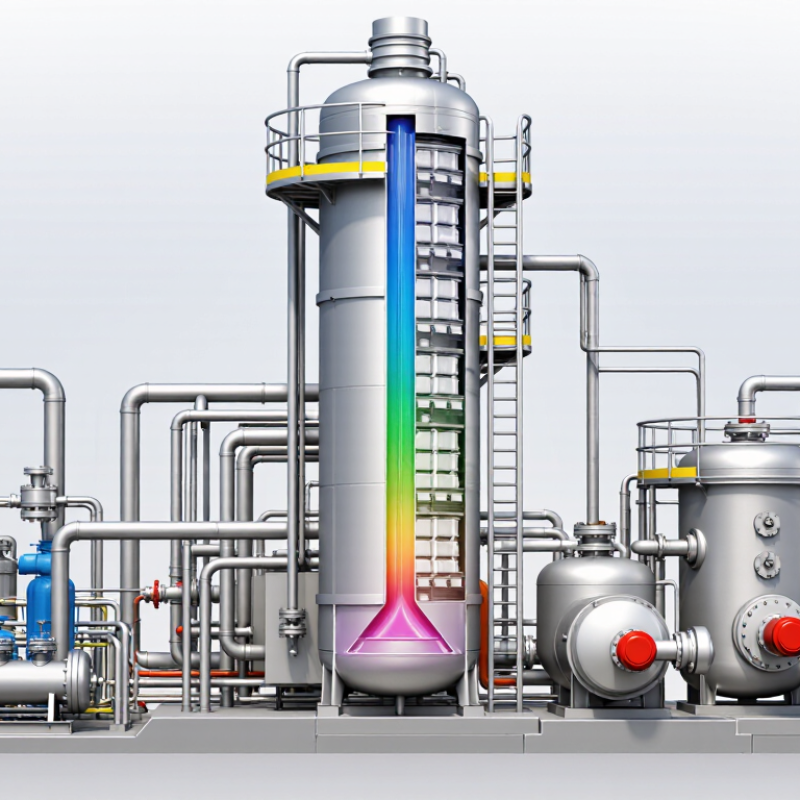
Before choosing an alcohol recovery tower, define what actually enters it. Take representative samples during normal operation and during feed changes, then record temperature, pressure, and flow rate. Measure alcohol and water content, and note whether the sample separates or contains suspended material. Small details matter. A single clean sample may not reflect a full shift.
Water content affects the amount of liquid the tower must heat and separate. Solids can settle in piping or foul trays and packing, so record their concentration, particle size, and tendency to form deposits. A screen or filter may help, but it can also hide the solids load if sampling happens downstream. That is an easy mistake to make.
Trace impurities deserve careful measurement, even when present at low concentrations. Depending on their volatility and chemistry, they may leave with the overhead, remain in the bottoms, contribute to foaming, or create corrosion risks. Use suitable laboratory methods and report detection limits, not just “below limit.” Give the tower designer expected values and credible high and low ranges, rather than one average. If the feed varies sharply, more sampling—or a small process test—may be needed before equipment dimensions are fixed. Sampling itself is imperfect; I would revisit the data after startup.
Set Recovery Targets Around Ethanol’s 95.6 wt% Atmospheric Azeotrope
How to Choose an Alcohol Recovery Tower for Your Plant
Set Recovery Targets Around Ethanol’s 95.6 wt% Atmospheric Azeotrope
At atmospheric pressure, ethanol and water form an azeotrope near 95.6 wt% ethanol. A conventional distillation tower cannot exceed this concentration by simple distillation. That limit matters. Set the tower’s target around the actual feed composition, required ethanol recovery, and product specification—not an assumed maximum purity. If the process needs drier ethanol, plan a separate dehydration step and evaluate it with the tower as part of the full system.
For tower selection, compare operating pressure, feed rate, heat duty, and expected composition changes across the operating range. Ask for performance estimates at realistic conditions, including periods when feed quality shifts. A neat target can still rest on a poor sample; I have seen design discussions move too quickly past that detail. Measure, don’t assume. Confirm how the supplier defines recovery, product purity, and energy use, and check that these figures use the same basis. Small details matter.
Tips: Keep a recent feed analysis and identify the pressure basis for every purity target. Leave room for normal process variation, but avoid oversizing based on guesswork. Review the assumptions with operations staff before fixing the design point.
Size Tower Capacity Using Peak Feed Rate and 70–90% of Flood
For an alcohol recovery tower, use the highest credible feed rate, not the daily average. Check production records for short surges, startup periods, and batch transfers. A pump reading that peaks briefly may not represent a sustained load, but ignoring it can still cause unstable operation. That distinction matters.
Estimate vapor and liquid traffic at the peak rate, then compare the load with the tower’s predicted flood point. A practical target is often 70–90% of flooding at peak conditions. The lower end offers more room for feed swings, fouling, or uncertain data. The upper end may suit steadier service, but leaves less operating margin. Flooding is not a single fixed flow rate: pressure, temperature, alcohol concentration, and the selected trays or packing all affect capacity. Have the rating checked against the actual process conditions.
Leave room for real plant behavior. A warm feed can flash more vapor than expected; a partly blocked distributor can also create uneven flow. Not every upset is captured in a spreadsheet. Compare normal and peak cases, and confirm that the tower can turn down without losing separation. If feed measurements are rough, say so and size conservatively. That may mean a larger tower than the neat calculation suggests. The assumption deserves a second look.
Compare Tray and Packed Designs Using HETP and Efficiency Data
An alcohol recovery tower should be selected by comparing separation performance at the plant’s actual feed rate, pressure, and composition. For early screening, Kister’s Distillation Design and Perry’s Chemical Engineers’ Handbook report commonly used ranges of roughly 0.3–0.6 m HETP for structured packing and 0.5–0.9 m for random packing. These are starting points, not guarantees. Feed impurities, liquid distribution, and operating load can shift HETP significantly.
Tray designs are often assessed using Murphree vapor efficiency. Professional design references give approximate screening values of 50–80% for many tray applications, but the result depends on tray type and service. Trays may suit variable loads and provide easier inspection. Packing can reduce pressure drop, which matters under vacuum, but poor liquid distribution can erase its efficiency advantage. A neat HETP comparison is useful; it is not the whole design. Check capacity, pressure drop, turndown, fouling risk, and maintenance access against vendor-neutral test data or pilot results.
Tips: Compare data at matching pressure and throughput. Ask for the test basis behind each HETP or efficiency figure. A few misplaced liquid streams can matter more than a small difference in published values. And the first estimate may be wrong. That deserves a review.
Check Materials, Pressure Rating, and Heat Duty Against Plant Conditions
An alcohol recovery tower should be specified for the actual feed, not a generic service label. Check water content, trace acids, chlorides, cleaning chemicals, and startup temperatures before choosing the shell, internals, and gaskets. Stainless steel may suit many streams, but weld condition and local contaminants can change corrosion behavior. NACE International’s 2016 IMPACT study estimated global corrosion costs at US$2.5 trillion annually. It also estimated that better corrosion management could save 15–35%. These are broad industry figures, not a tower-life guarantee.
Set design pressure and temperature using credible upset cases, including blocked outlets and control failures. Confirm the code basis and relief assumptions with the vessel engineer. Check heat duty against feed rate, composition, fouling, and utility temperatures. The U.S. Department of Energy’s process-heating sourcebook estimates that process heating uses about 51% of manufacturing energy. That sector-wide figure cannot replace a site-specific heat balance. Conditions change. Small details matter.
Tips: Compare duty at minimum and peak throughput. Request material certificates, corrosion allowance, weld inspection records, and pressure-vessel calculations. Leave room for uncertainty; a clean design basis does not guarantee clean operating conditions.